- Introduction to Optical Sorters for Plastic Recycling
- Technological Innovation in the Recycling Sector
- The Origins of Optical Sorters: A Path of Evolution
- How Optical Sorters Work: From Theory to Practice
- Advantages of Optical Sorters in the Recycling Process
- How to Evaluate Your Needs to Choose the Right Machine
- The Technological Differences Between the Various Models of Sorters
- Final Considerations for an Informed Purchase
Discover How to Choose the Most Suitable Optical Sorter for Your Production Needs by Analyzing Technologies, Features, and Offerings from Leading Recycling Industry Manufacturers
by Marco Arezio
The growing focus on environmental issues and the need for sustainable waste management have led to the development of advanced recycling technologies, with a particular emphasis on plastic. One of the most significant innovations in plastic recycling is the optical sorter, a machine designed to identify and separate recycled plastic flakes based on visual and chemical characteristics.
These machines have transformed the recycling process, increasing efficiency and improving the quality of recycled materials. In this article, we will explore the history of optical sorters, their functionality, key manufacturers, and the benefits they offer to the recycling industry.
The Origins of Optical Sorters: Who Invented Them?
Optical sorters are the result of decades of research and innovation in industrial automation and artificial vision. The idea of using optical technology for material separation dates back to the 1970s when the first technologies for automated sorting using optical sensors were developed, initially applied in the agricultural industry for sorting grains and fruits. However, it was not until the 1990s that these technologies began to be applied to the recycling industry, responding to the growing demand for more efficient methods to separate recyclable materials.
Pioneering companies that started developing and commercializing optical sorters for recycling include TOMRA Sorting Solutions, Sesotec, and Pellenc ST. These companies introduced advanced technologies such as optical and X-ray sensors to identify and separate various types of plastics, metals, and other materials from waste, improving the purity of recovered materials and reducing waste.
How Optical Sorters Work
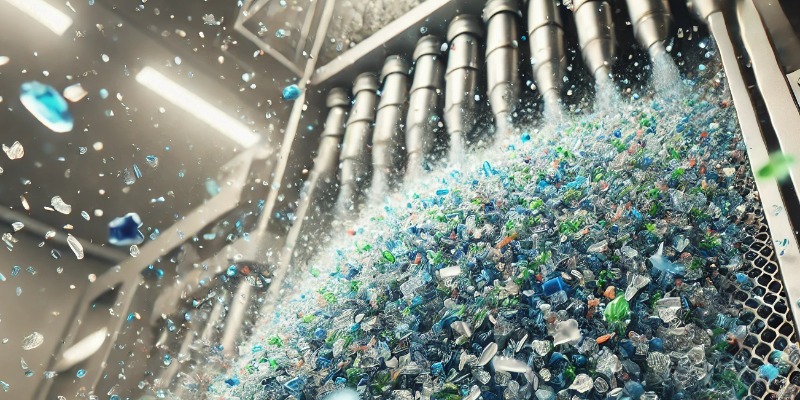
The operation of optical sorters relies on the use of complex sensors and algorithms that analyze the visual, chemical, or physical properties of materials. In the case of plastic recycling, flakes—small pieces of shredded plastic—are analyzed based on color, transparency, chemical composition, and other detectable characteristics.
The main steps in the operation of an optical sorter are as follows:
Feeding and Distribution
Shredded plastic material is loaded into the machine and evenly distributed on a conveyor belt, which carries it to the detection area.
Detection
In the detection phase, optical or infrared sensors scan the moving flakes. Depending on the machine, different types of sensors may be used:
Color sensors: Analyze the visible color of the flakes to separate materials with different colorations.
Infrared sensors (NIR): Used to identify the chemical composition of materials, as they can detect differences in the molecular structure of various types of plastic, such as PET, HDPE, PP, etc.
X-ray sensors: Used to detect contamination by metallic materials or to distinguish materials with different densities.
Selection and Separation
Once the flakes are detected and analyzed, an ejection system (usually consisting of compressed air jets) separates the materials based on preset criteria. The air jets propel the flakes into different collection channels, thus separating pure materials from impurities.
Benefits of Optical Sorters in Industrial Recycling
The introduction of optical sorters has revolutionized the plastic recycling industry for several reasons:
Increased Material Purity: Optical sorters enable the production of plastic flakes with a high level of purity, reducing the presence of contaminants such as other types of plastic, metals, or non-recyclable materials. This is crucial for producing high-quality recycled plastics suitable for applications such as food packaging.
Higher Operational Efficiency: By automating the sorting process, recycling companies can process large quantities of material in less time, increasing productivity and reducing operational costs.
Waste Reduction: Optical sorters allow for the recovery of a greater amount of recyclable material, minimizing waste that would otherwise end up in landfills or incinerators.
Flexibility in Sorting: Machines can be programmed to separate different types of plastics and quickly adapt to changes in waste streams, making them ideal for facilities that handle mixed materials or those sourced from various origins.
The Leading Manufacturers of Optical Sorters
Over the years, several manufacturers have established themselves as leaders in the field of optical sorters for plastic recycling. The main players include:
TOMRA Sorting Solutions: A global leader in optical sorting, TOMRA offers a range of machines for plastic sorting based on NIR technology and color sensors. Their machines, such as the AUTOSORT series, are renowned for their high efficiency and precision in material separation.
Sesotec GmbH: This German company specializes in separation solutions for various industrial sectors, including the plastic recycling industry. Sesotec produces optical sorters that use NIR and X-ray sensors for accurate separation of plastic materials.
Pellenc ST: A French company that has developed a wide range of optical sorters for the recycling sector. Their machines are recognized for their ability to combine different sensors (NIR, visible, and X-ray) to achieve multifunctional material sorting.
Steinert GmbH: Based in Germany, Steinert specializes in magnetic and optical separation solutions. Their optical sorters are used in both metal and plastic recycling, with a particular focus on achieving high-purity material separation.
Differences Between Machines from Various Manufacturers
The primary differences among the optical sorters offered by various manufacturers lie in the sensor technology used, energy efficiency, and operational flexibility. For instance:
TOMRA is known for its high-precision NIR sensors.
Sesotec stands out for integrating X-ray sensors capable of detecting metallic contaminants.
Pellenc ST is renowned for its flexible solutions that allow the combination of multiple sensor types in a single machine, offering greater versatility in the sorting process.
Another distinguishing factor is the machines' ability to handle different volumes of material. For example, TOMRA’s machines are designed for large-scale facilities requiring high processing capacity, while other companies, such as Sesotec, offer modular solutions suitable for smaller-scale operations.
Conclusions
Optical sorters have revolutionized the plastic recycling industry by making the sorting process more efficient and sustainable. With these technologies, companies can produce high-quality recycled materials, reduce waste, and enhance the overall sustainability of their operations.
Technological advancements and competition among leading manufacturers continue to improve the performance of these machines, making them more accessible and versatile.
For companies looking to invest in optical sorters, it is essential to carefully analyze their production needs, considering factors such as the types of materials processed, production volume, and available budget.
Choosing the right manufacturer and the most suitable machine can make a significant difference in operational efficiency and return on investment. In a constantly evolving market, relying on cutting-edge technologies and experienced partners can ensure a winning strategy—for business success and a positive environmental impact.
© All Rights Reserved